
Working Environment Check
Clear plastic scraps, sundries around the injection machine and mould mounting area. Keep operation passages unobstructed. Remove oil, raw material particles on the floor to prevent slipping. Keep flammable materials far away from high-temperature mould zone.
Mechanical Structure Check
Verify mould locking components, guide pins, ejector system, cooling circuit and pin valve assemblies are fastened without looseness. Check mould clamping surface for damage, foreign matter and burrs. Confirm safety guard, emergency stop buttons, travel limit switches and mould protection sensors work normally.
Hot Runner & Pin Valve System Check
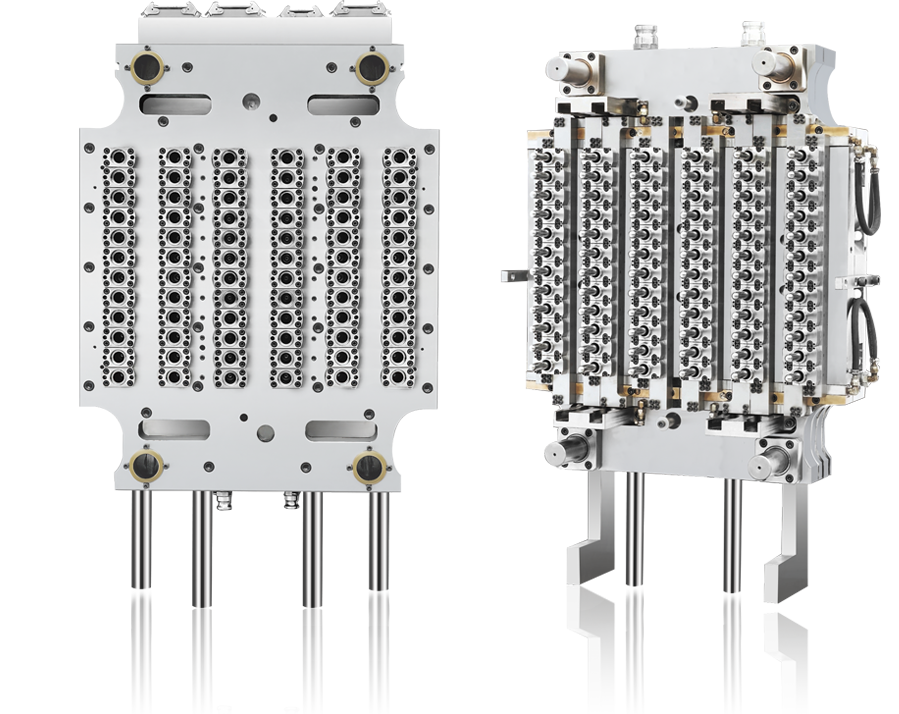
Inspect pin valve nozzles, valve pins, heating bands and thermocouples. Ensure no heating element damage, wiring aging. Check hot runner sealing surface to avoid melt leakage. Confirm pin valve opening & closing action is smooth without jamming.
Cooling Circuit Check
Check water pipelines for leakage, blockage and aging. Ensure cooling water pressure and flow reach specified requirements. Prevent insufficient cooling leading to mould deformation and product defects.
Electrical System Check
Control cabinet stays dry and dust-free. Check earthing connection reliability. Confirm all temperature control modules operate normally.
Operator PPE Confirmation
Wear heat-resistant work clothes, anti-slip safety shoes and heat-proof gloves. Tie up long hair. Avoid wearing ornaments. Equip dry powder fire extinguishers within accessible range.
Standard startup sequence: Install and lock mould → Connect cooling water → Switch on hot runner temperature control → Heat up to preset temperature with heat preservation → Conduct low-speed mould trial clamping → Test pin valve movement → Perform trial injection, start mass production after sample confirmation.
Never place hands or body parts between mould halves during clamping and ejection. Do not reach into hot runner and gate area.
Adjustment of pin valve timing, ejection stroke and mould parameters should be carried out after stopping injection movement whenever possible.
Observe mould running status continuously. Watch for abnormal noise, melt leakage, unbalanced filling and pin valve stuck issues. Stop operation immediately once abnormal conditions appear.
Unified communication signals are required for multi-person cooperation. Any staff can trigger the emergency stop button in case of danger. It is forbidden to short-circuit or shield safety interlock devices.
Do not rinse mould, hot runner heater and electric control components directly with water.
Normal shutdown procedure: Stop injection → Empty residual melt inside hot runner → Reduce mould temperature gradually → Open mould and clean cavity → Cut off heating power → Close cooling water → Disconnect main power supply.
Mould disassembly, cleaning cavity, maintenance of pin valve components must be implemented after machine shutdown and power cut. Implement lockout-tagout procedure, hang warning sign "Mould Maintenance, Do Not Start".
Regularly lubricate guide pins, ejector pins and sliding components with dedicated lubricant. Prevent lubricant contamination to mould cavity.
After long-term production, clean pin valve nozzle and flow channel to avoid carbon deposition causing valve pin jamming. For long-term storage, perform rust prevention treatment on mould surfaces.
High-temperature scald: Rinse wound with continuous cold water; seek medical treatment for severe burns.
Mechanical pinch/crush injury: Shut down equipment immediately. Stop bleeding and dress wound; send patient to hospital for serious injury.
Electric shock: Cut off main power supply first. Do not touch the victim directly before power cut, then carry out rescue work.
Do not remove or shield safety guards, emergency stop switches, mould protection interlock devices.
Do not put hands into mould clamping area during machine operation.
Do not conduct mould maintenance, pin valve disassembly while power and heating are switched on.
Do not run mould with deformed valve pin, damaged sealing parts or serious carbon deposition.
Do not set excessive injection pressure and clamping force beyond mould design specification.
Untrained personnel are forbidden to disassemble hot runner pin valve system and modify core process parameters.
Do not operate the mould with unresolved faults.
พบบริษัท Foshan Yongyute Precision Machinery Co.,Ltd
ในปี 2551 เป็นองค์กรครบวงจรที่เชี่ยวชาญด้าน
ทำระบบฉีดขวด PET และระบบเป่า
เกี่ยวกับ


ลิขสิทธิ์ @Foshan Yongyute Precision Machinery Co.,Ltd. สงวนลิขสิทธิ์. การสนับสนุนด้านเทคนิค: การออกแบบทิศทางทั่วไป
แผนผังไซต์เว็บไซต์นี้ใช้คุกกี้เพื่อให้แน่ใจว่าคุณได้รับประสบการณ์ที่ดีที่สุดบนเว็บไซต์ของเรา


 English
 Español
 Portugues
 Pусский
 Français
 العربية
 Türk dili
 Indonesia
 Tiếng Việt



 Phone
ความคิดเห็น
(0)